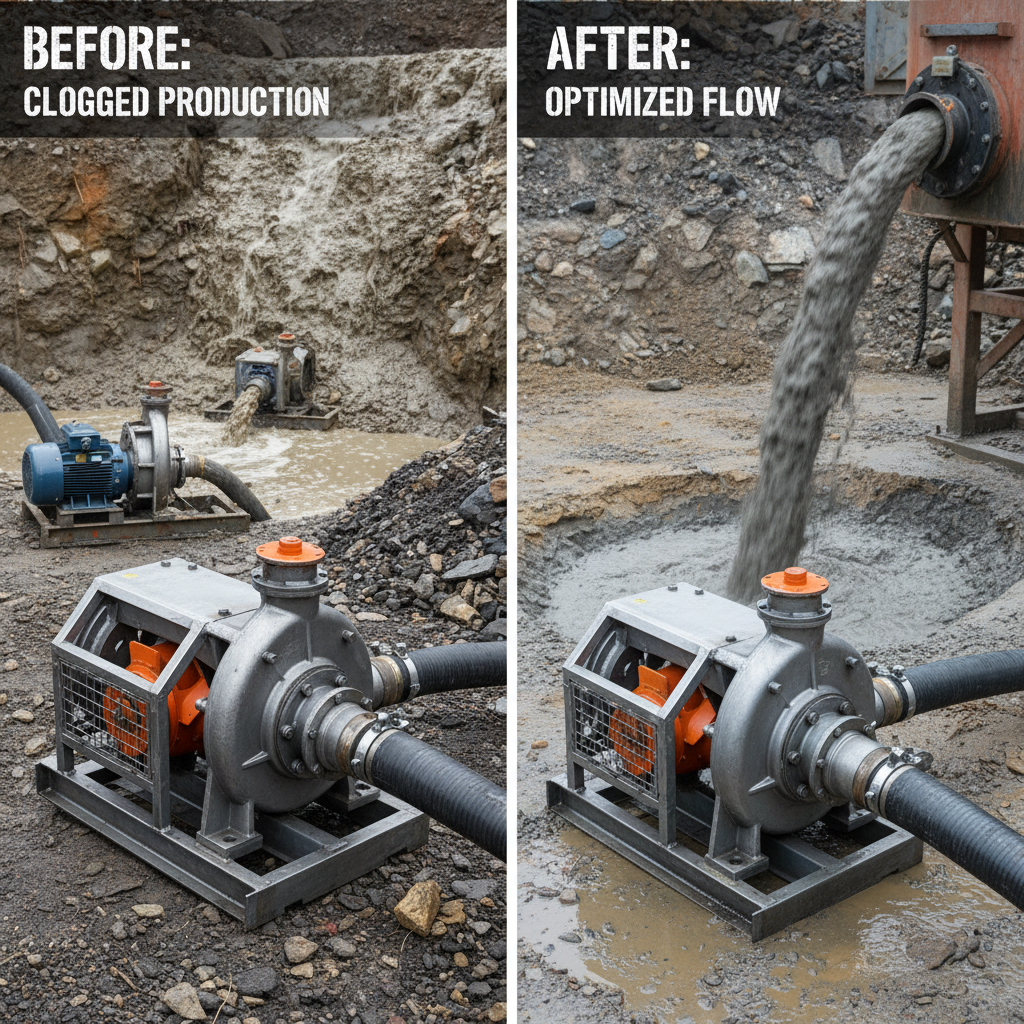
Managing the transport of tenacious froth and abrasive materials presents a significant challenge in global mining and metallurgical operations. The need for a specialized heavy duty sludge pump has become paramount as industries push for higher efficiency in processing copper, alumina, and various ores. Understanding the mechanics of froth handling is essential for preventing system downtime and maintaining a continuous production flow in harsh industrial environments.
Across the globe, the demand for robust fluid handling solutions is rising due to the increasing complexity of mineral processing. Standard pumps often fail when faced with high-viscosity liquids and corrosive slurries, leading to costly maintenance cycles and operational bottlenecks. By implementing a high-performance heavy duty sludge pump, companies can ensure the reliable transportation of difficult media while protecting their infrastructure from premature wear.
The VFD series vertical froth duty slurry pump is specifically engineered to bridge the gap between standard pumping and the extreme requirements of the mining sector. By utilizing a vertical structure and a double-case design, this heavy duty sludge pump allows operators to adjust parameters according to the media, ensuring that corrosive or abrasive slurries containing froth are moved swiftly and efficiently.
Engineering Design of the VFD Vertical Pump
The VFD series is designed as a heavy-duty vertical pump specifically to handle difficult and tenacious froth. By employing a vertical structure, this heavy duty sludge pump minimizes the footprint required for installation while maximizing the gravitational assist for material inflow. The design incorporates a tangential inlet, which allows the media to flow into the pump swiftly, effectively removing excess froth and preventing air-locks.
Furthermore, the inclusion of a spill box ensures that any extra materials are returned to the pond, preventing overflow and maintaining a stable operational environment. The double-case design is a critical feature, granting users the flexibility to adjust the centrifugal pump settings based on the specific characteristics of the media being transported, whether it be copper mining tailings or alumina slurry.
Core Components for Maximum Durability
Reliability in a heavy duty sludge pump depends heavily on the quality of its bearing system. The VFD series utilizes TV, TVR, and PNL bearings, with the bearing body securely attached to the motor cabinet or motor frame. This configuration ensures structural stability and reduces vibration during the transport of abrasive materials.
To combat the corrosive nature of metallurgical and mining slurries, the pump's bins are constructed from a combination of high-quality stainless steel and steel plates. These are further reinforced with rubber linings to provide an extra layer of protection against wear and chemical erosion, extending the service life of the equipment significantly.
The drive system offers versatility through both direct and indirect drive options. Indirect drive systems make it considerably easier for users to replace belts and adjust rotation speeds. This flexibility allows the operator to fine-tune the pump's performance in real-time, adapting to the actual working conditions of the sludge being processed.
Handling High Viscosity and Froth Challenges
In mining operations, two primary obstacles often hinder productivity: the presence of froth and the handling of high-viscosity liquids. A standard pump often struggles with these properties, leading to cavitation or complete blockage. This is where the specialized design of a heavy duty sludge pump becomes essential.
The VFD series addresses these issues by combining a tangential inlet for swift material flow with a robust vertical structure. By managing the froth before it enters the main impeller chamber, the heavy duty sludge pump maintains a consistent flow rate even when dealing with the most tenacious froth found in copper and alumina mining.
Through the use of rubber linings and a double-case centrifugal design, the pump can be optimized for the specific density of the slurry. This ensures that high-viscosity liquids are moved without excessive energy loss, making the heavy duty sludge pump a critical asset for ore processing plants.
Performance Metrics in Industrial Applications
Evaluating the efficiency of a heavy duty sludge pump requires looking at its ability to maintain throughput across different industries. From coal chemical plants to paper and pulp making, the VFD series demonstrates a high capacity for handling corrosive slurries while maintaining structural integrity.
The ability to adjust rotation speeds via the belt system allows for a wide performance range, ensuring that the pump can handle varying concentrations of solids without overloading the motor. This adaptability is key to reducing operational costs and increasing the overall lifecycle of the pumping unit.
Efficiency Ratings of Slurry Pump Configurations
Versatile Industry Implementations
The application of a heavy duty sludge pump extends far beyond basic mining. In city planning and water conservancy, these pumps are used to manage sewage and environmental protection projects. Their ability to handle non-clogging materials makes them ideal for architecture and fire protection systems where reliability is non-negotiable.
Furthermore, the petroleum and chemical industries rely on these units to move corrosive byproduct slurries. In the medicine and electric power sectors, the precision and durability of the VFD series ensure that hazardous waste or cooling slurries are transported without leakage, adhering to strict safety and environmental regulations.
Long-term Operational Value and Efficiency
Investing in a professional heavy duty sludge pump provides tangible long-term value through reduced maintenance and energy savings. The use of cost-effective manufacturing processes combined with high-grade materials ensures that the total cost of ownership remains low over the equipment's lifespan.
The ease of belt replacement in indirect drive models means that downtime is kept to a minimum. This operational continuity is vital for large-scale mining sites where a pump failure can halt an entire production line, leading to significant financial losses.
By integrating a double-case design, the pump allows for the replacement of wear parts without dismantling the entire system. This innovation ensures that the heavy duty sludge pump remains in peak condition, providing a win-win scenario for operators and owners alike.
Technical Comparison of Material Selection
The choice of materials is the most critical factor in determining the longevity of a heavy duty sludge pump. Depending on the chemical composition of the froth, users can choose between stainless steel for corrosion resistance or rubber lining for maximum abrasion resistance.
Steel frameworks provide the necessary rigidity to support the vertical motor and bearing assembly, ensuring that the pump does not shift or vibrate under heavy loads. This structural integrity is what allows the VFD series to maintain its performance in the most demanding environments.
Ultimately, the combination of high-quality steel plates and precision-engineered bearings creates a heavy duty sludge pump that is capable of operating 24/7 in the most aggressive slurry conditions found in modern ore processing.
Material and Performance Analysis for VFD Slurry Pumps
|
Material Type
|
Abrasion Resistance
|
Corrosion Rating
|
Typical Application
|
| Rubber Lining |
10/10 |
8/10 |
High-Abrasive Ore |
| Stainless Steel |
6/10 |
10/10 |
Chemical Sludge |
| Steel Plate |
7/10 |
5/10 |
General Mining |
| Composite Alloy |
9/10 |
7/10 |
Copper Froth |
| Chromium Steel |
8/10 |
6/10 |
Alumina Ore |
| Hybrid Lining |
9/10 |
9/10 |
Mixed Industrial Waste |
FAQS
The VFD series is superior because it combines a vertical structure with a tangential inlet and a spill box. This specific configuration allows the pump to remove excess froth and handle high-viscosity liquids effectively, preventing the air-locking and clogging that typically plague standard centrifugal pumps in mining environments.
The double-case design provides the flexibility to adjust the pump according to the specific media being processed. It allows operators to maintain the pump more efficiently and tailor the performance to the density and abrasiveness of the sludge, reducing the frequency of complete system teardowns during maintenance.
Yes, the VFD series is designed for both corrosive and abrasive slurries. By utilizing quality stainless steel and rubber linings, the pump can resist chemical erosion while simultaneously handling the physical wear of heavy sludge, making it suitable for the chemical industry and metallurgical plants.
Indirect drive allows users to easily replace belts and adjust the rotation speed of the pump based on real-time working conditions. This is critical when the viscosity of the sludge changes, as it allows the operator to optimize energy consumption and pump flow without replacing the motor.
While copper and alumina mining are primary users, this pump is also widely used in coal chemicals, paper and pulp making, water conservancy, and petroleum. Any industry dealing with high-viscosity, froth-filled, or abrasive liquids will benefit from the VFD series' specialized design.
These specific bearings are engineered to handle the high axial and radial loads associated with vertical pumping of heavy materials. By attaching the bearing body directly to the motor cabinet or frame, the system ensures maximum stability and minimal vibration, which significantly extends the life of the internal components.
Conclusion
The VFD series vertical froth duty pump represents a significant advancement in the transport of tenacious and abrasive materials. By integrating a tangential inlet, rubber-lined components, and a flexible drive system, it addresses the core challenges of froth and high viscosity that typically hinder mining and industrial operations. Its ability to be customized via a double-case design ensures that it remains a versatile and reliable heavy duty sludge pump for a wide array of demanding applications.
As global mining and industrial processing move toward greater automation and sustainability, the need for low-maintenance, high-efficiency pumping solutions will only grow. Investing in a professional, cost-effective pumping system not only secures operational continuity but also enhances the overall safety and productivity of the plant. We invite you to explore our full range of solutions and establish a win-win cooperation. Visit our website: www.kingmechpump.com