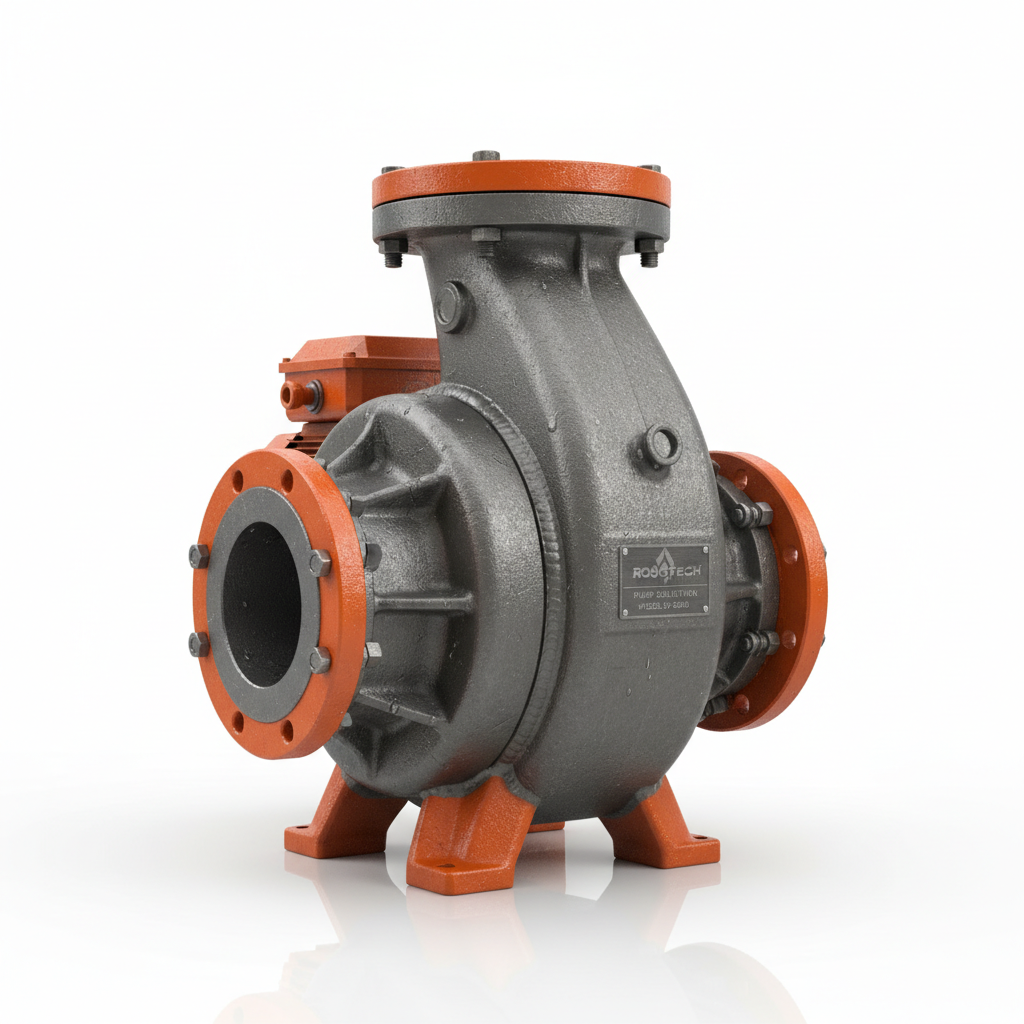
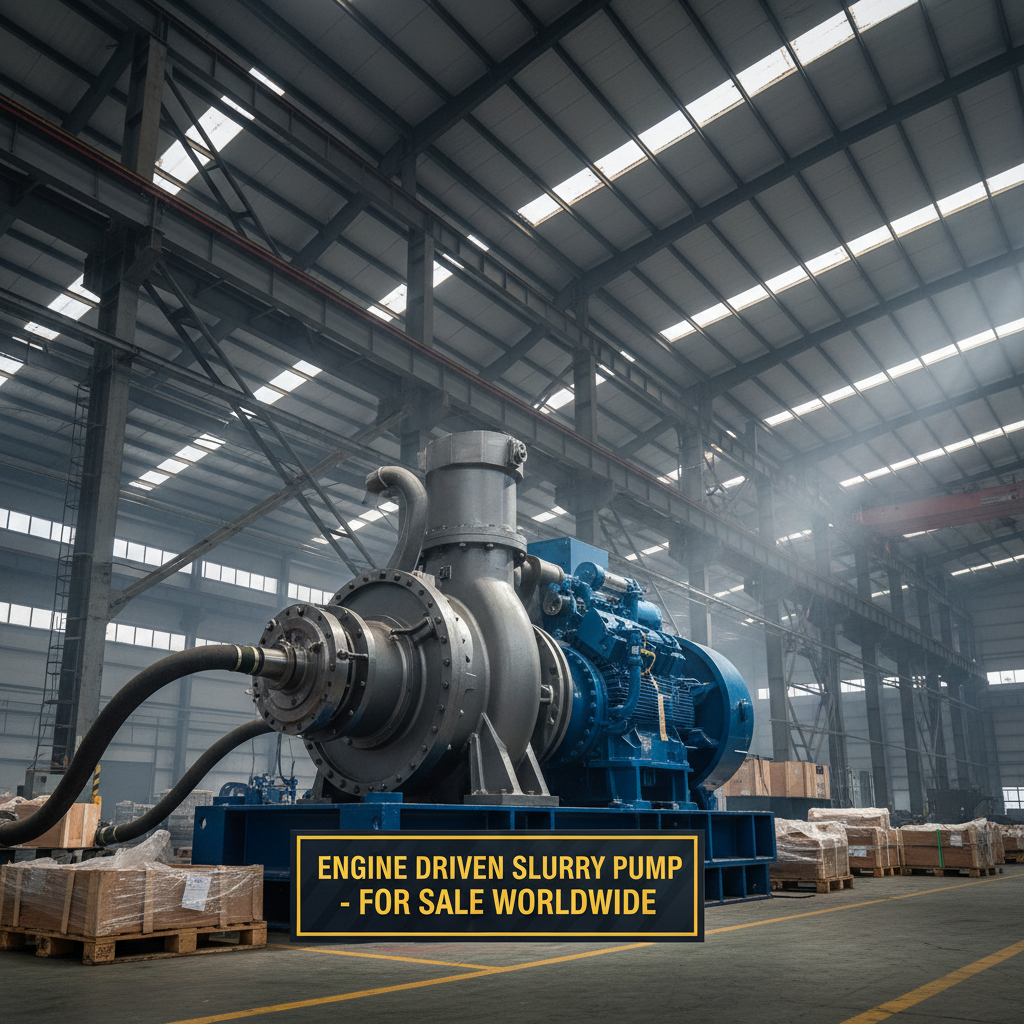
In the demanding world of industrial fluid transport, the movement of abrasive materials presents a constant battle against wear and equipment failure. A heavy duty slurry pump is specifically engineered to handle these grueling conditions, ensuring that thick, particulate-laden liquids are moved efficiently without compromising the integrity of the machinery. From mining operations to chemical processing, the ability to maintain steady flow rates while resisting internal erosion is the cornerstone of operational uptime.
Globally, the reliance on robust pumping solutions has increased as the demand for raw minerals and refined chemicals grows. Industrial standards, including those aligned with ISO guidelines, emphasize the need for equipment that minimizes maintenance intervals and maximizes energy efficiency. The challenge lies in balancing the high velocity required for transport with the need to reduce the abrasive impact of particles against the pump casing and impeller.
By integrating advanced hydraulic designs and wear-resistant materials, a heavy duty slurry pump provides the reliability necessary for high-capacity industrial cycles. These machines are not merely tools but critical infrastructure components that prevent costly shutdowns in sectors like gold mining, alumina production, and potash extraction.
Engineering Design for Maximum Wear Resistance
The core of any heavy duty slurry pump lies in its configured volute design. By optimizing the volute cross-section, the casing material is strategically distributed at the points of maximum wear. This is particularly critical when transporting larger particles, as it ensures that the high-impact zones are reinforced, extending the overall lifespan of the pump shell.
Furthermore, the implementation of a Low V open cutwater design significantly lowers slurry velocity at the discharge point. By reducing this velocity, the pump minimizes consequential wear and prevents the separation of fluids at flows less than the Best Efficiency Point (BEP). This results in a more forgiving operating range and a broader efficiency band, allowing the pump to maintain performance across varying flow conditions.
Hydraulic Efficiency and Flow Dynamics
Achieving high efficiency in a slurry environment requires a deep understanding of turbulence. Patented impeller wear ring profiles are used to reduce wear on the throatbush and impeller by restricting recirculation and dampening turbulence. This ensures that the energy delivered by the motor is converted into fluid movement rather than wasted through internal eddies.
The use of a unique extended shroud impeller design further enhances this efficiency. By trapping pump-out vane tip vortices against the shroud, the design prevents the further development of vortices that would otherwise cause significant side-liner wear. This containment of flow ensures a more linear and predictable hydraulic path.
Additionally, the profiled impeller tip is engineered to increase the radial velocity of flow in the center of the vane. This prevents inward spiral flow, which is a common cause of premature casing wear. By directing the slurry more effectively, the pump maintains high volumetric efficiency even when dealing with high-density solids.
Advanced Component Protection Strategies
Protecting the internal surfaces of a heavy duty slurry pump is essential for reducing the total cost of ownership. One such innovation is the "Tear drop" frame liner. This unique insert shape ensures that any local side wall wear occurs on the replaceable liner rather than on the more expensive pump casing, allowing for cheaper and faster repairs.
For the most aggressive applications, flat ceramic wear resistant inserts are available as an option. These inserts provide an impenetrable barrier against highly abrasive particles, ensuring that the heavy duty slurry pump can operate in extreme environments where standard alloys would erode rapidly.
The synergy between the one-piece robust frame and the cartridge-type bearing assembly provides the structural rigidity needed to handle the heavy loads associated with slurry transport. This ensures that the shaft remains perfectly aligned, reducing vibration and further protecting the pump's internal components from mechanical stress.
Maintenance Accessibility and Serviceability
Operational downtime is the enemy of productivity in mining and industrial plants. To combat this, the heavy duty slurry pump incorporates a unique "T-liner" and spigotted fits, which ensure that all internal components can be assembled and disassembled with ease. The casing is further equipped with three shackle lifting points to facilitate safe and rapid movement during overhaul.
Flexibility in configuration is also a key feature. A gland seal pump can be easily converted to a centrifugal seal by adding an expeller and a new shaft sleeve. This allows operators to upgrade their sealing technology based on the specific demands of their slurry without needing to replace the entire pump unit.
Operational Efficiency Ratings by Pump Component
Global Industrial Applications and Use Cases
The versatility of the heavy duty slurry pump makes it indispensable across various global industries. In the mining sector, it is used extensively for moving sand and gravel, gold, and copper ores. The ability to handle high solids concentrations allows mines to transport material efficiently from the pit to the processing plant.
Beyond mining, these pumps are critical in the production of alumina, phosphate, and potash. In these chemical-heavy environments, the pump must resist both abrasion and corrosion. The same robust design is also applied in the sugar industry and for transporting ash or dust in power plants, proving its adaptability to a wide range of particulate matter.
Sealing Performance and Dry Run Capabilities
Sealing is one of the most common failure points in industrial pumps. To address this, the heavy duty slurry pump utilizes deep and efficient impeller pump-out vanes combined with high-ratio (85%) expeller diameters. This configuration produces exceptional dry sealing performance, preventing slurry from leaking into the bearing housing.
The leading edge of the expelling vane features a patented shape designed specifically to reduce tip turbulence. By maximizing the pressure reduction and sealing effect, the pump can operate reliably even under conditions that would typically cause seal failure in standard pumps.
This focus on sealing integrity ensures that the cartridge-type bearing and shaft assembly remain protected from contamination. The external impeller adjustment mechanism further supports this by allowing operators to maintain the correct clearance without dismantling the pump, ensuring the seal remains optimal.
Material Selection for Aggressive Environments
Choosing the right material for a heavy duty slurry pump is a balance between hardness and toughness. While high-chrome alloys are standard for abrasion resistance, the addition of specialized liners allows the pump to adapt to specific chemical profiles. The goal is to ensure that the sacrificial components wear out predictably and can be replaced without affecting the main structure.
In applications involving potash or phosphate, the materials must resist corrosive salts while still withstanding the physical impact of solids. The engineered distribution of material in the volute ensures that the thickest sections of the casting are located where the slurry velocity is highest, providing a logical defense against erosion.
Ultimately, the integration of patented shapes, from the "T-liner" to the profiled impeller, creates a system that manages wear rather than simply fighting it. This scientific approach to material placement and flow management defines the modern standard for slurry transport.
Analysis of Material Performance in Heavy Duty Slurry Pump Applications
| Application Material |
Wear Resistance Score |
Corrosion Resistance |
Typical Lifespan (Months) |
| High Chrome Alloy |
9/10 |
Moderate |
12-18 |
| Ceramic Inserts |
10/10 |
Excellent |
24-36 |
| Standard Rubber Liner |
6/10 |
High |
6-12 |
| Hardened Steel |
7/10 |
Low |
8-14 |
| Duplex Stainless |
8/10 |
Very High |
18-24 |
| Composite Polymer |
5/10 |
High |
6-10 |
FAQS
A heavy duty slurry pump is specifically designed with abrasion-resistant materials and specialized hydraulic geometries, such as configured volutes and profiled impellers. Unlike standard pumps, it is built to handle high concentrations of solids without rapid erosion, utilizing sacrificial liners and robust frames to maintain structural integrity under extreme abrasive stress.
The Low V open cutwater design reduces the velocity of the slurry as it exits the impeller. Since wear is exponentially related to velocity, lowering the speed at the cutwater significantly reduces the erosion rate. Additionally, it prevents flow separation at lower flow rates, broadening the efficiency band and reducing turbulence-induced wear.
Yes, thanks to the high-ratio expeller diameter and efficient pump-out vanes, these pumps offer exceptional dry sealing performance. The design creates a pressure barrier that prevents leakage and protects the bearings, although prolonged dry running is generally avoided to maximize the life of the seals.
The "T-liner" is a specialized replaceable wear component designed to protect the pump casing. By ensuring that wear occurs on the liner rather than the main casting, it allows for easier and cheaper maintenance. The spigotted fits ensure that these liners can be replaced quickly during scheduled shutdowns.
Industries dealing with abrasive solids are the primary beneficiaries. This includes mining (gold, copper, iron), chemical processing (potash, phosphate, alumina), and power generation (fly ash removal). Any application where water is mixed with grinding particles requires this level of heavy-duty engineering.
Impeller clearance should be checked periodically during routine maintenance. Because the pump features an external adjustment mechanism below the bearing housing, clearance can be optimized without dismantling the pump, ensuring the pump maintains peak efficiency as the impeller wears down over time.
Conclusion
The implementation of a heavy duty slurry pump is a strategic investment in operational reliability. By combining advanced volute configurations, patented impeller profiles, and innovative sealing technology, these pumps transform the challenge of abrasive transport into a manageable industrial process. The focus on maintenance accessibility—through T-liners and external adjustment mechanisms—ensures that the cost of ownership remains low while productivity remains high.
Looking forward, the evolution of slurry pumping will likely lean toward even more advanced ceramic composites and digital monitoring to predict wear in real-time. For any operation involved in mining or chemical processing, prioritizing a pump that balances hydraulic efficiency with extreme durability is the only way to ensure long-term sustainability. Visit our website for more professional solutions: www.kingmechpump.com